Oct 12, 2026
Custom rotational molding manufacturers
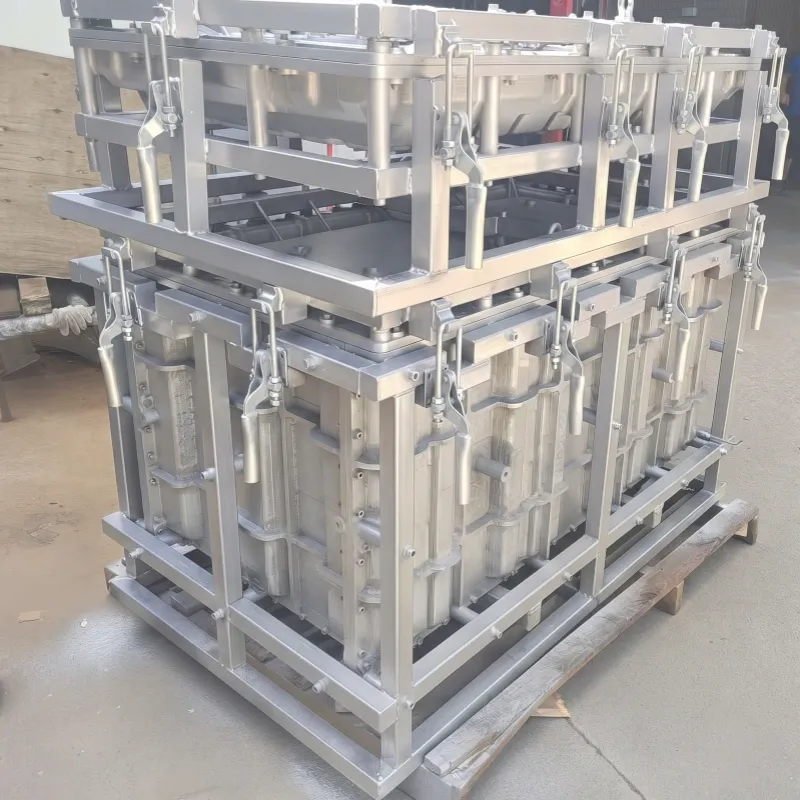
Common Defects in Rotational Molding Mold Design and How to Solve Them
Rotational molding, often called rotomolding, is a unique plastic manufacturing process that produces hollow, seamless parts with uniform wall thickness. From large storage tanks and kayaks to playground equipment and medical devices, this method has carved out a significant niche in the plastics industry. However, like any manufacturing process, rotomolding comes with its own set of challenges. In this post, we will explore the most common mold design defects in rotational molding and practical solutions to address them.
Wall Thickness Variation
One of the most persistent issues in rotomolding is inconsistent wall thickness. While rotomolding generally achieves excellent uniformity across complex geometries, certain factors can cause thin spots or thick sections that compromise part performance.
Sharp corners, abrupt thickness transitions, and narrow sections are common culprits. Internal mold corners with small radii tend to heat and cool more slowly than adjacent walls, resulting in thinner material in those areas. Conversely, outside corners with small radii heat and cool more rapidly, often producing thicker walls.
The solution lies in thoughtful design. Generous radii and gradual transitions between thicknesses allow heat to distribute more evenly. Designers who incorporate smooth, balanced shapes from the outset can significantly improve wall consistency. For areas where thicker walls are needed, making the mold wall thinner or using a higher thermal conductivity metal in that region can help.
Bridging in Double-Wall Parts
Bridging occurs when parallel walls within a mold are positioned too close together. The plastic powder cannot flow freely between them, creating a solid bridge of material that blocks complete cavity filling. The result is a defective part with a discontinuous wall structure—one section may be thinner than intended or missing entirely.
The industry standard solution is straightforward: maintain a separation between parallel walls of at least five times the nominal wall thickness. While separations as narrow as three times the wall thickness have been molded successfully, such tight tolerances require exceptional process control and may not yield consistent results.
Powder quality also plays a role. Poor dry flow characteristics can promote bridging, especially as the powder heats and its flow properties deteriorate. Using high-quality powder with verified flow characteristics is essential for problematic geometries.
Warpage and Dimensional Instability
Warpage remains one of the most significant unresolved challenges in rotational molding. It is primarily caused by differential shrinkage during cooling—when different sections of the part cool at different rates, internal stresses develop and the part distorts.
Research has shown that cooling rate directly influences warpage, shrinkage, and residual stress. The faster the cooling, the greater the warpage tendency across different polymers. Rapid external cooling creates temperature gradients that cause the part to pull away from the mold wall unevenly, initiating bending stresses.
Controlled cooling is the most effective countermeasure. Slower, more uniform cooling allows the part to solidify gradually, minimizing internal stress buildup. Mold pressurization has also emerged as a promising technique—holding the part against the mold wall during cooling helps prevent the gap formation that leads to warpage.
Porosity and Bubbles
Internal bubbles and surface pinholes are common in rotomolded parts. As powder particles melt and coalesce, air pockets become trapped in the polymer melt. These voids act as crack initiation sites and can cause brittle failures, particularly in low-temperature impact tests.
Insufficient cooking time is a frequent cause—if the part is not heated long enough to allow bubbles to escape, they remain trapped in the wall. However, overcooking introduces its own risks: thermal degradation of the polymer can make the material inherently brittle.
Monitoring internal air temperature is the most reliable way to optimize the cooking cycle. A peak internal air temperature (PIAT) of 375-425°F is typically recommended for polyethylene, though suppliers should be consulted for specific resin grades.
Poor Powder Flow and Incomplete Filling
Complex mold geometries with deep cavities or restricted sections can impede powder flow. When the depth of a cavity exceeds its width, heat transfer to the bottom becomes restricted, resulting in thin walls at the deepest points.
Stationary baffles on the mold surface can improve heat distribution for cavities with depth-to-width ratios below 0.5. For deeper cavities, forced air venturis are recommended to ensure adequate heating reaches the cavity bottom. Insulation pads applied to specific areas can also help manage thickness by reducing heat transfer where less material is desired.
Conclusion
Rotational molding offers remarkable design freedom and produces stress-free, seamless parts that serve countless industries. By understanding these common defects—wall thickness variation, bridging, warpage, porosity, and powder flow issues—designers and manufacturers can take proactive steps during mold design and process optimization. Generous radii, proper wall separation, controlled cooling, and temperature monitoring are the cornerstones of defect-free rotomolding. When these principles are applied consistently, the process delivers the durable, high-quality parts that have made rotomolding a trusted manufacturing method for over seven decades.